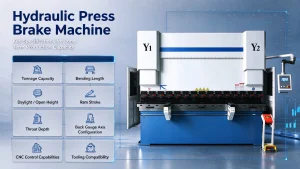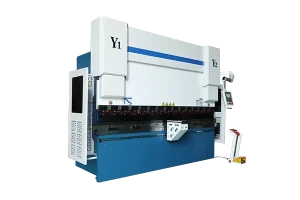
A hydraulic press brake machine is a significant capital investment, so selecting the right specifications is important for long-term production capacity and bending performance. Key specifications include tonnage capacity, bending length, daylight or open height, ram stroke, throat depth, back gauge axis configuration, CNC control capabilities, and tooling compatibility. Each factor affects how the machine handles different materials, part sizes, bending sequences, and production requirements.
For buyers, evaluating these specifications together provides a clearer picture of whether a hydraulic press brake machine can handle current work orders and support future production needs.
9 Specifications You Should Check
1、Tonnage Capacity
Tonnage determines the maximum material thickness you can bend at a given length. Required tonnage depends on material type, thickness, bend length, and V-die opening width.
How to calculate: The standard formula is:
P = (575 × t² × L) / V
Where P = tonnage (kN), t = material thickness (mm), L = bend length (m), V = V-die opening (mm, typically 8× material thickness).
| Material | Tonnage Factor vs. Mild Steel |
| Mild steel (reference) | 1.0 |
| Stainless steel | 1.5–1.6 |
| Aluminum (6061-T6) | 0.4–0.5 |
| Brass | 0.6–0.7 |
Practical check: If you bend 4 mm mild steel across a full 2 m length, you need approximately 80–100 tons. Always add a 20–30% safety margin — running a machine at maximum rated tonnage continuously accelerates seal and pump wear.
2、Bending Length
Bending length is the maximum distance over which the machine can apply full tonnage. It must exceed your longest required part, but oversizing adds cost without benefit.
Practical check: Measure your longest workpiece flange plus 100–200 mm for tooling clearance. Common ranges:
| Application | Typical Bending Length |
| Enclosure panels, electronics | 1.0–1.6 m |
| General fabrication | 2.0–3.0 m |
| Construction, structural parts | 3.0–4.0 m |
| Heavy industry, large enclosures | 4.0–6.0 m+ |
Key point: Bending length should match tonnage. A 3 m machine rated at only 80 tons cannot bend thick plate across the full bed — tonnage drops near the edges due to frame deflection.
3、Daylight and Open Height
Daylight (open height) is the distance between the top of the lower die and the underside of the upper tool at maximum ram up position. This determines the maximum flange depth you can form in one stroke.
Practical check: Your required flange height + tool height + material thickness must be less than daylight. Insufficient daylight forces multi-stroke bending, reducing throughput and accuracy.
Typical daylight ranges: 200–400 mm on standard machines, 400–600 mm on deep-throat models.
4、Ram Stroke
Ram stroke is the vertical travel distance of the upper beam. Too short a stroke prevents deep-box forming; too long reduces cycle speed.
Practical check: Required stroke = tool clearance + material thickness + flange depth + 50 mm safety margin. For shallow pans and brackets, 100–150 mm stroke is sufficient. For deep boxes, 200+ mm may be required.
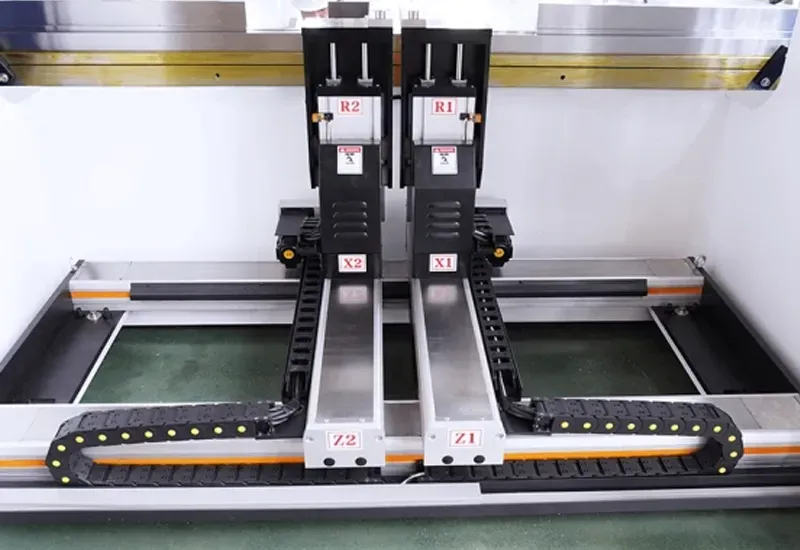
5、Back Gauge Axis Configuration
The back gauge positions the workpiece before bending, controlling flange dimension. More axes provide greater positioning flexibility.
| Axes | Movement | Best For |
| X | Front-to-back | Standard single-bend parts |
| X + R | Adds vertical finger adjustment | Varying material thickness, multi-stage bending |
| X + R + Z1 + Z2 | Adds independent lateral left/right | Asymmetrical parts, multi-flange sequences |
CNC back gauge positioning repeatability is typically ±0.01 mm with ball screw and linear guide construction.
6、Throat Depth
Throat depth is the distance from the vertical frame upright to the centerline of the lower die. It limits how deep into the sheet you can form a bend — critical for large panels and channel sections.
Practical check: Throat depth must exceed the deepest reverse flange or return bend on your parts. Standard throat depths range from 200–300 mm; deep-throat machines offer 400+ mm.
7、Control System
The CNC control system determines programming capability, angle compensation, and production efficiency. Key functions to verify:
- Graphic programming: Can operators draw or import DXF files directly?
- Angle calculation: Does the system auto-calculate tonnage and back gauge position from material properties?
- Tool library: Can tooling profiles be stored and recalled?
- Offline programming: Can programs be created on a PC and transferred via USB or network?
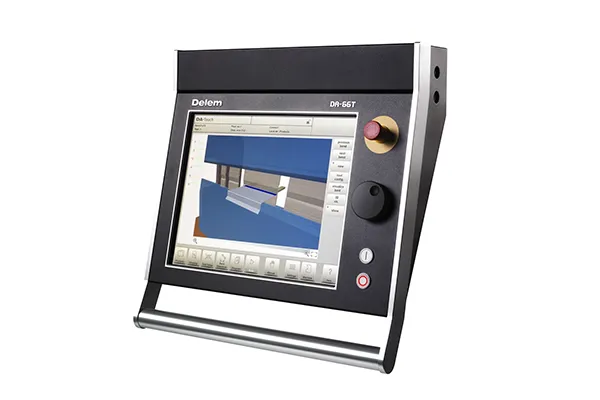
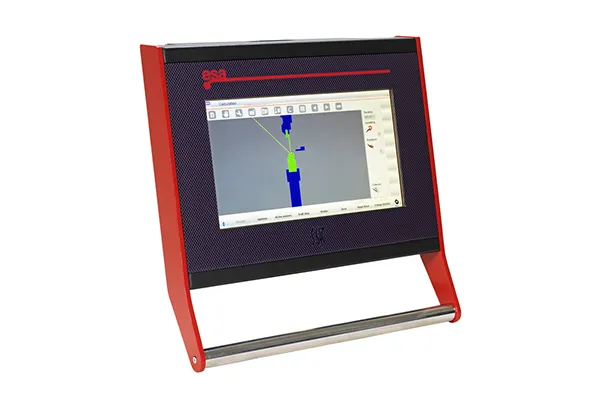
Common controllers: Delem (DA-41T, DA-52T, DA-66T), ESA, Cybelec. Each supports different axis counts and programming depth.
8、Tooling Compatibility
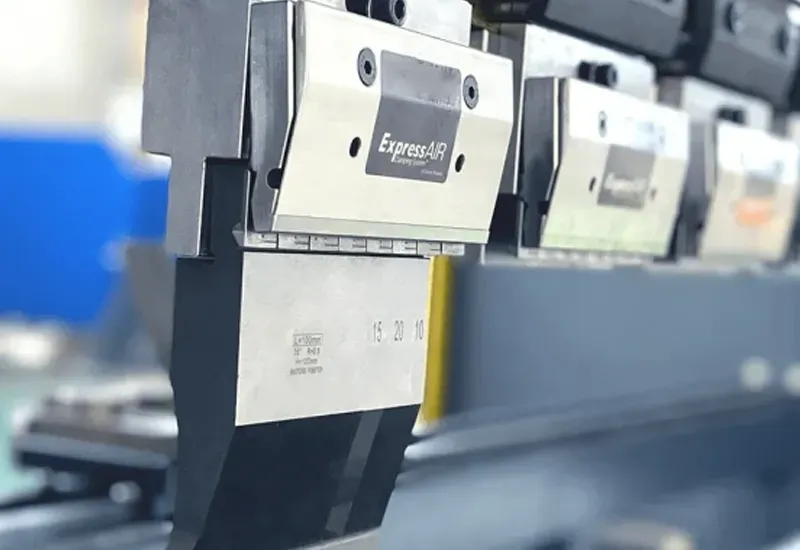
Press brake tooling follows different clamping standards (American Precision, European Precision, Wila). Verify that the machine’s clamping system matches your existing tools or planned tooling purchases.
Prateral check:
- Upper tool clamp type (manual or hydraulic quick-clamp)
- Lower tool holder section width (commonly 55 mm or 80 mm)
- Tool segment set availability for partial bending
9、Frame Rigidity and Deflection
Under full tonnage, every press brake frame deflects slightly. The amount of deflection affects bend angle consistency across the full length. Look for:
- Synchro system: Hydraulic or electro-hydraulic servo synchronization keeps ram parallel under asymmetric loads. Typical ram parallelism: ±0.02 mm.
- Crowning: Mechanical or hydraulic crowning compensates for frame deflection. Without crowning, the center of a long bend opens up by 0.5–1.5° vs. the ends.
FAQs about Hydraulic Press Brake Machine
How much tonnage do I need for a hydraulic press brake?
Calculate using P = (575 × t² × L) / V, then add 20–30% safety margin. For 3 mm mild steel at 2 m, you need ~60–80 tons.
What is the difference between bending length and bed length?
Bending length is the distance over which full tonnage can be applied. Bed length is the physical machine frame length, which is slightly longer for tooling overhang.
Do I need a CNC back gauge for simple parts?
For single-bend, low-volume work, a manual back gauge may suffice. For repeat production, multi-step bending, or tight flange tolerances (±0.1 mm), CNC is essential.
What is crowning and why does it matter?
Crowning compensates for frame deflection under load, keeping the bend angle consistent across the full length. Without it, the center of a long part bends 0.5–1.5° less than the ends.
Hydraulic vs electric press brake — which should I choose?
Hydraulic press brakes handle higher tonnage (100+ tons) and are more cost-effective for heavy plate. Electric servo presses offer faster cycle speeds and lower energy use but are typically limited to lighter gauge work.
Conclusion
The right hydraulic press brake machine depends on your actual production requirements — not maximum spec numbers. Tonnage, bending length, daylight, stroke, back gauge axes, throat depth, control system, and tooling compatibility must all match your workpiece dimensions and material range. Provide your supplier with sample part drawings, material specifications, and expected production volume to ensure the machine is configured correctly.
Need help matching press brake specifications to your production requirements? Contact us for configuration guidance and batch pricing.